
Peristaltic Pump Tubing Selection: Material Properties, Performance Factors, and How to Get It Right
Views: 0 Author: Kevin Fang Publish Time: 2026-05-28 Origin: Chensheng Medical
Table of Contents
Peristaltic pumps are deceptively simple machines. A rotor compresses a flexible tube against a housing, and fluid moves forward. No valves, no seals, no fluid contact with the pump mechanism. In theory, the only consumable is the tubing.
In practice, the tubing is everything.
The wrong tubing choice — wrong material, wrong hardness, wrong dimensions, wrong curing chemistry — will cause flow rate drift, premature tube failure, failed biocompatibility testing, or all three simultaneously. In pharmaceutical manufacturing, IV drug delivery, or clinical diagnostics, any of these failures carries serious consequences: batch rejection, patient safety incidents, or regulatory action.
This guide gives you the complete technical framework for selecting peristaltic pump tubing — covering material science, mechanical performance, dimensional requirements, fluid compatibility, and the qualification process that separates a reliable supply from an expensive mistake.

How Peristaltic Pumps Work — And Why Tubing Properties Are Critical
Understanding tubing selection starts with understanding what the pump actually does to the tubing.
In a peristaltic pump, the rotor rollers or shoes compress the tubing to approximately 50–60% of its original inner diameter with each pass. The tubing must then fully recover to its original geometry before the next compression cycle. This compression-recovery cycle repeats continuously — in high-speed laboratory pumps, this can mean hundreds of thousands of cycles per day.
The tubing's ability to recover fully and consistently after each compression determines:
Flow accuracy — incomplete recovery means less fluid displaced per cycle, causing flow rate to drift downward over time
Tube service life — fatigue failure (cracking, spallation, wall thinning) occurs when the tubing cannot elastically absorb the repeated deformation
Particle generation — degraded tubing sheds microscopic particles into the fluid stream — a critical concern in pharmaceutical and clinical applications
Pump calibration stability — a pump calibrated at installation will drift out of calibration as the tubing fatigues
Every material property discussed in this guide connects directly to one or more of these performance outcomes.
Material Options for Peristaltic Pump Tubing
Several elastomeric materials are used in peristaltic pump tubing. Each has a distinct performance profile:
Material | Compression Set | Chemical Resistance | Biocompatibility | Temp Range | Typical Application |
Platinum-cured silicone | Excellent (≤10%) | Good (aqueous, mild acids/bases) | Excellent — USP Class VI, ISO 10993 | –60°C to +200°C | Pharmaceutical, medical, biotech |
Peroxide-cured silicone | Moderate (15–25%) | Good | Variable — depends on post-cure | –50°C to +180°C | Industrial, non-critical applications |
C-Flex / TPE | Good | Moderate | Good | –70°C to +135°C | Single-use bioprocessing |
Tygon (PVC-based) | Moderate | Good | Acceptable (plasticizer concerns) | 0°C to +65°C | General laboratory |
Norprene / Santoprene | Good | Excellent (solvents, oils) | Moderate | –60°C to +135°C | Chemical processing |
Natural rubber (latex) | Poor | Poor | Problematic (latex allergy) | 0°C to +80°C | Legacy applications only |
PTFE / fluoropolymer | Poor (rigid) | Excellent | Excellent | –200°C to +260°C | Not suitable for peristaltic pumping |
Why Platinum-Cured Silicone Dominates Medical and Pharmaceutical Peristaltic Applications
For any peristaltic pump application involving patient contact, pharmaceutical fluid transfer, or regulated bioprocessing, platinum-cured silicone is the material of choice — and for good reason:
Superior compression set recovery — the defining performance requirement for peristaltic tubing
Zero extractables from curing by-products — critical for drug-contact and patient-contact fluid paths
Broad temperature range — compatible with autoclave sterilization (121°C / 134°C) and cryogenic storage
Consistent lot-to-lot biocompatibility — no variable residual peroxide decomposition products
Regulatory acceptance — USP Class VI and ISO 10993 compliance is standard, not optional
For a detailed comparison of platinum-cured vs. peroxide-cured silicone chemistry and why it matters for biocompatibility, see: Platinum-Cured vs. Peroxide-Cured Silicone: Which Should You Choose?
The Five Critical Material Properties for Peristaltic Pump Tubing
1. Compression Set — The Most Important Property
Compression set measures how much permanent deformation a material retains after being compressed for a defined time and temperature. It is expressed as a percentage:
Compression Set (%)=t0−trt0−ts×100Compression Set (%)=t0−tst0−tr×100
Where:
t0t0 = original thickness
trtr = thickness after recovery
tsts = compressed thickness
A compression set of 0% means perfect recovery. A higher percentage means more permanent deformation.
For peristaltic pump tubing, the practical implication is direct:
Compression Set | Effect on Pump Performance |
< 10% (platinum-cured silicone) | Minimal flow drift; long tube life; stable calibration |
10–20% | Moderate flow drift over time; acceptable for non-critical applications |
> 20% | Significant flow drift; frequent recalibration required; shorter tube life |
> 35% | Rapid tube failure; unacceptable for regulated applications |
Standard test method: ASTM D395 Method B (compressed 25% for 22 hours at 70°C or 100°C).
✅ Chensheng Medical platinum-cured silicone pump tubing achieves compression set ≤ 8% (ASTM D395, 22h/70°C) — consistently across production lots.
2. Shore A Hardness — Balancing Pumpability and Durability
Shore A hardness determines how much force the pump rotor must exert to compress the tubing, and how the tubing responds to repeated compression.
Too soft (Shore A < 40):
Tubing collapses too easily — rollers may over-compress, causing wall-to-wall contact and flow interruption
Reduced fatigue life — soft tubing deforms more per cycle, accelerating wear
Dimensional instability — soft tubing is harder to extrude to tight tolerances
Too hard (Shore A > 70):
Pump motor must work harder — increased energy consumption and motor wear
Higher contact stress at roller/tubing interface — accelerated surface fatigue
Reduced flexibility — tubing may kink in pump head during installation
Optimal range for most peristaltic pump applications: Shore A 50–65
Application | Recommended Shore A |
Low-flow precision dosing (laboratory) | 50–55 |
Standard IV / pharmaceutical fluid transfer | 55–65 |
High-pressure peristaltic (industrial bioprocess) | 60–70 |
Gentle cell culture / shear-sensitive fluids | 40–50 |
Your pump manufacturer's documentation will typically specify the recommended tubing hardness range for their pump head design. Always verify compatibility before substituting tubing.
3. Tensile Strength and Elongation at Break
These properties determine the tubing's resistance to mechanical failure under the stresses of peristaltic pumping:
Tensile strength (minimum 7 MPa for medical pump tubing) — resistance to tearing at the roller contact zone
Elongation at break (minimum 400%) — ability to deform without cracking; higher elongation correlates with better fatigue life
For platinum-cured medical silicone pump tubing, typical values are:
Tensile strength: 8–11 MPa
Elongation at break: 500–650%
These values should be confirmed on the material's Technical Data Sheet (TDS) and verified on lot-specific Certificates of Analysis (CoA).
4. Tear Resistance
Tear resistance (measured per ASTM D624 or ISO 34) is particularly important for pump tubing because the roller contact creates stress concentrations at the tubing wall. Low tear resistance leads to:
Crack initiation at the inner wall surface (the highest-stress zone)
Progressive crack propagation through the wall — leading to tubing failure and fluid leakage
Particle generation from torn inner wall material
Minimum acceptable tear resistance for medical pump tubing: 25 kN/m (ASTM D624 Die C)
Chensheng Medical platinum-cured pump tubing achieves ≥ 30 kN/m — providing a meaningful safety margin above the minimum threshold.
5. Surface Finish and Inner Wall Quality
The inner wall surface of peristaltic pump tubing is in direct contact with the fluid being pumped. Surface quality affects:
Particle generation — rough inner walls shed particles into the fluid stream
Biofilm formation — surface irregularities provide attachment sites for microorganisms
Extractables profile — surface area affects the rate of leachable migration into the fluid
Cleanability — smooth surfaces are easier to flush and clean between uses
For pharmaceutical and medical applications, inner wall surface roughness (Ra) should be ≤ 1.6 μm. Chensheng Medical's extrusion process consistently achieves Ra ≤ 0.8 μm on medical pump tubing inner walls.
Dimensional Requirements and Tolerances
The Three Critical Dimensions
Every peristaltic pump tubing specification is defined by three dimensions:
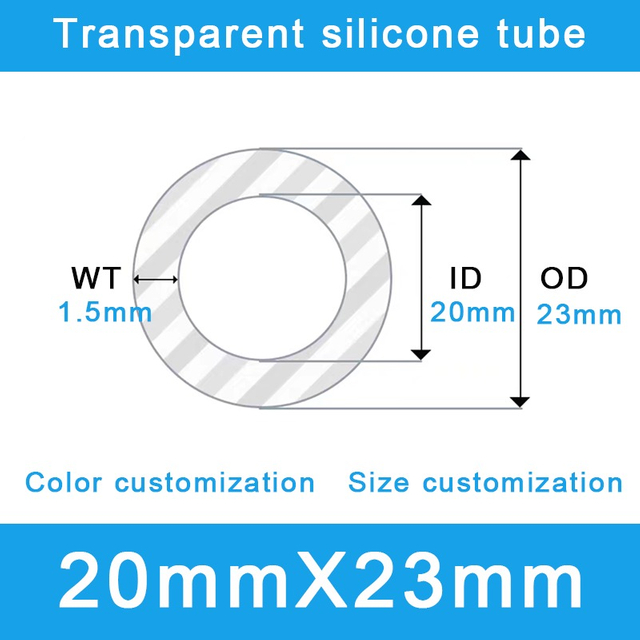
Inner Diameter (ID) — determines flow rate per revolution; directly affects pump calibration
Outer Diameter (OD) — determines fit in the pump head; affects compression ratio
Wall Thickness (WT) — determines compression set behavior, fatigue life, and pressure rating
The relationship between these dimensions is:
Wall Thickness=OD−ID2Wall Thickness=2OD−ID
Why Dimensional Tolerance Is Non-Negotiable
In a peristaltic pump, flow rate is directly proportional to the internal cross-sectional area of the tubing. A small variation in ID produces a proportional variation in flow rate:
ID Variation | Flow Rate Impact |
±0.1mm on a 3.0mm ID tube | ±6.7% flow rate variation |
±0.05mm on a 3.0mm ID tube | ±3.3% flow rate variation |
±0.025mm on a 3.0mm ID tube | ±1.7% flow rate variation |
For pharmaceutical dosing applications where ±2% accuracy is required, dimensional tolerance on the tubing ID is a primary accuracy driver — not just a quality metric.
Chensheng Medical Dimensional Tolerance Standards
Dimension | Standard Tolerance | Precision Tolerance (on request) |
Inner Diameter (ID) | ±0.10 mm | ±0.05 mm |
Outer Diameter (OD) | ±0.10 mm | ±0.05 mm |
Wall Thickness (WT) | ±0.10 mm | ±0.05 mm |
Precision tolerance (±0.05mm) is standard for all medical and pharmaceutical pump tubing orders. Achieving this tolerance requires:
Precision-ground extrusion dies with controlled land length
Closed-loop dimensional monitoring during extrusion (laser micrometer)
Temperature-controlled extrusion environment
Controlled post-extrusion cooling to prevent dimensional relaxation
Standard Pump Tubing Size Compatibility
Chensheng Medical produces pump tubing compatible with all major peristaltic pump platforms, including:
Pump Platform | Compatible Tubing Sizes Available |
Watson-Marlow (various models) | 0.5mm–12.7mm ID |
Masterflex (Cole-Parmer) | 0.8mm–15.9mm ID |
Ismatec (IDEX) | 0.25mm–8.0mm ID |
Longer Pump | 0.5mm–10mm ID |
Custom / OEM pump heads | Any ID/OD/WT to specification |
If your pump is not listed, contact our applications engineering team with the pump model and required tubing size — we will confirm compatibility or develop a matched specification.
Fluid Compatibility Considerations
Platinum-cured silicone has excellent compatibility with a wide range of fluids encountered in medical and pharmaceutical peristaltic pump applications:
Fluid Category | Silicone Compatibility | Notes |
Aqueous solutions (saline, buffer, water) | ✅ Excellent | No swelling or degradation |
Dilute acids (pH > 2) | ✅ Good | Concentrated HF and H₃PO₄ attack silicone |
Dilute bases (pH < 12) | ✅ Good | Concentrated NaOH causes surface degradation |
Alcohols (ethanol, IPA) | ✅ Good | Minor swelling at high concentrations |
Pharmaceutical APIs (aqueous) | ✅ Excellent | Verify E&L compatibility for specific APIs |
Cell culture media | ✅ Excellent | Low extractables critical for cell viability |
Blood and blood products | ✅ Good | Verify hemocompatibility per ISO 10993-4 |
Aromatic hydrocarbons (toluene, xylene) | ⚠️ Poor | Significant swelling — use fluoropolymer tubing |
Chlorinated solvents (DCM, chloroform) | ⚠️ Poor | Significant swelling — use fluoropolymer tubing |
Concentrated oxidizing acids | ❌ Not compatible | Use PTFE or fluoropolymer |
Silicone oils | ⚠️ Variable | May cause swelling depending on viscosity |
For pharmaceutical applications: Always conduct an extractables and leachables (E&L) compatibility study for your specific drug formulation and tubing lot before clinical or commercial use. Even with platinum-cured silicone, certain APIs may interact with silicone extractables at trace levels. For guidance on the certification framework governing extractables, see: USP Class VI, ISO 10993, and FDA 21 CFR 177.2600: Which Medical Silicone Certification Do You Actually Need?
Sterilization Compatibility
Many peristaltic pump applications in medical and pharmaceutical settings require sterile tubing or tubing that can be sterilized in-line or between uses.
Sterilization Method | Platinum-Cured Silicone Compatibility | Notes |
Autoclave (121°C, 15 min) | ✅ Excellent | No dimensional change; multiple cycles supported |
Autoclave (134°C, 3 min) | ✅ Excellent | Preferred for prion inactivation protocols |
Ethylene oxide (EtO) | ✅ Excellent | Requires adequate aeration post-sterilization |
Gamma irradiation (25–50 kGy) | ✅ Good | Minor yellowing possible at high doses; mechanical properties maintained |
Electron beam (E-beam) | ✅ Good | Similar to gamma; faster processing |
Chemical (peracetic acid, H₂O₂) | ✅ Good | Verify concentration and contact time |
UV irradiation | ⚠️ Surface only | Not a validated sterilization method for tubing |
Dry heat (180°C) | ✅ Excellent | Silicone withstands dry heat sterilization |
Important: Sterilization validation should be performed on your specific tubing lot and sterilization protocol. Dimensional and mechanical property verification post-sterilization is recommended as part of your qualification protocol.
Tube Life and Failure Modes: What to Expect and How to Extend It
Typical Tube Life
Peristaltic pump tubing is a consumable — it will eventually fatigue and require replacement. Typical service life depends on:
Pump speed (RPM) — higher speed = more compression cycles per unit time = shorter tube life
Occlusion setting — tighter occlusion (more compression) accelerates fatigue
Tubing hardness — softer tubing deforms more per cycle; harder tubing generates more contact stress
Fluid temperature — elevated temperature accelerates silicone fatigue
Tubing quality — dimensional consistency and material quality are the primary determinants of life variability
As a general benchmark for platinum-cured silicone pump tubing:
Pump Speed | Typical Tube Life |
Low speed (< 50 RPM) | 2,000–5,000 hours |
Medium speed (50–150 RPM) | 500–2,000 hours |
High speed (> 150 RPM) | 200–800 hours |
These are indicative ranges. Actual life depends heavily on pump model, occlusion setting, and operating conditions. We recommend establishing tube life empirically under your actual operating conditions as part of your qualification protocol.
Common Failure Modes and Root Causes
Failure Mode | Appearance | Most Likely Root Cause |
Spallation | Black or white particles in fluid | Inner wall fatigue; material quality issue |
Cracking (inner wall) | Visible cracks on inner surface | High compression set; fatigue; wrong hardness |
Wall thinning | Reduced wall thickness at roller contact zone | Normal wear; accelerated by high occlusion |
Kinking | Permanent bend in tubing | Tubing too soft; improper installation |
Flow rate drift | Decreasing flow rate over time | High compression set; tubing fatigue |
Tubing rupture | Sudden loss of flow; fluid leak | End-of-life fatigue failure; over-occlusion |
Surface stickiness | Tacky outer surface | Inadequate post-cure (peroxide-cured material) |
Swelling | Increased OD; reduced flow accuracy | Chemical incompatibility with pumped fluid |
If you are experiencing any of these failure modes with your current tubing supply, contact our applications engineering team — we can help diagnose the root cause and recommend the appropriate specification change.
How to Qualify Peristaltic Pump Tubing: A Practical Protocol
Switching pump tubing suppliers — or qualifying a new tubing specification — requires a structured qualification protocol. Here is the framework we recommend:
Step 1: Dimensional Verification (Incoming Inspection)
Measure ID, OD, and wall thickness on a statistically valid sample from each lot (minimum 10 pieces)
Verify all dimensions are within specification tolerance
Reject any lot where more than 1% of pieces fall outside tolerance
Step 2: Material Property Verification
Verify Shore A hardness against specification (±3 Shore A acceptable)
Request lot-specific CoA confirming tensile strength, elongation, and compression set
Verify curing system (platinum-cured) via material documentation
Step 3: Biocompatibility Documentation Review
Confirm ISO 10993-5 cytotoxicity report is current and covers the specific compound
Confirm USP Class VI report is current and covers the specific compound
Confirm 21 CFR 177.2600 compliance statement is available
For pharmaceutical applications: confirm extractables data is available
Step 4: Functional Performance Testing
Install tubing in your pump at standard occlusion setting
Run pump at operating speed for 30 minutes to allow break-in
Measure flow rate at 0h, 24h, 72h, 168h (1 week), and 500h
Acceptable flow rate drift: ≤ 3% over 500 hours for precision dosing applications
Step 5: Sterilization Compatibility Verification
Run samples through your actual sterilization protocol (3 cycles minimum)
Re-measure ID, OD, wall thickness post-sterilization
Verify no dimensional change > 1% and no visual degradation
Step 6: Accelerated Life Testing (for critical applications)
Run pump continuously at 1.5× normal operating speed
Inspect tubing at defined intervals for cracking, wall thinning, and spallation
Establish failure mode and time-to-failure as a basis for replacement interval

Chensheng Medical Peristaltic Pump Tubing: Technical Specifications
Property | Specification | Test Method |
Curing system | Platinum-catalyzed addition cure | Material documentation |
Shore A hardness | 50, 55, 60, 65 (standard grades) | ASTM D2240 |
Tensile strength | ≥ 8.5 MPa | ASTM D412 |
Elongation at break | ≥ 500% | ASTM D412 |
Tear resistance | ≥ 30 kN/m | ASTM D624 Die C |
Compression set | ≤ 8% (22h / 70°C) | ASTM D395 Method B |
ID tolerance | ±0.05 mm (precision grade) | Laser micrometer |
OD tolerance | ±0.05 mm (precision grade) | Laser micrometer |
Wall thickness tolerance | ±0.05 mm (precision grade) | Laser micrometer |
Inner wall roughness (Ra) | ≤ 0.8 μm | Profilometer |
Temperature range | –60°C to +200°C | — |
Biocompatibility | USP Class VI · ISO 10993-5 · ISO 10993-10 | Full reports available |
Regulatory | FDA 21 CFR 177.2600 · ISO 13485 | Documentation available |
Available ID range | 0.25 mm – 25 mm | Custom sizes available |
Standard lengths | 1m, 5m, 10m, 25m, 50m coils | Custom lengths available |
Colors | Clear (standard) · custom colors available | FDA-compliant pigments |
For custom OEM pump tubing — specific ID/OD/wall combinations, custom hardness, custom colors, or private label packaging — see our complete OEM process guide: Custom Medical Silicone Products: The Complete OEM/ODM Process From Concept to Delivery
Frequently Asked Questions (FAQ)
Q1: How do I know which tubing size to order for my specific pump model?
A: Most pump manufacturers publish a tubing compatibility chart specifying the required ID, OD, and wall thickness for each pump head model. If you have the pump model number, our applications engineering team can confirm the correct tubing specification. Alternatively, send us a sample of your current tubing and we will measure and match it.
Q2: Can your pump tubing replace OEM tubing from the pump manufacturer?
A: In most cases, yes. Our tubing is manufactured to the same dimensional specifications as OEM pump tubing, using equivalent or superior platinum-cured silicone compounds. Many customers switch to Chensheng Medical tubing as a cost-effective alternative to OEM-branded tubing without any change in pump performance. We recommend running our qualification protocol (described above) before switching in a regulated application.
Q3: What is the minimum order quantity for peristaltic pump tubing?
A: For standard catalog sizes (common ID/OD/wall combinations), we can supply from as little as 10 meters for initial qualification. For custom sizes requiring new extrusion tooling, minimum order quantities depend on the tooling investment — our team will advise at quotation stage. Production orders are typically priced per meter with volume discounts from 100m, 500m, and 1,000m+.
Q4: Do you supply pump tubing pre-cut to specific lengths, individually packaged?
A: Yes. We offer value-added processing including cut-to-length, individual packaging, lot labeling, and sterile packaging (EtO or gamma sterilized). For single-use pump sets incorporating silicone tubing as a component, we can also supply tubing pre-assembled with connectors or fittings. Contact our team to discuss your specific packaging requirements.
Q5: How should peristaltic pump tubing be stored to maximize shelf life?
A: Store tubing in its original packaging in a cool (15–25°C), dry environment away from direct sunlight, UV sources, ozone-generating equipment, and solvents. Do not store tubing under compression or in a kinked position. Under these conditions, shelf life for platinum-cured silicone pump tubing is 3–5 years from the date of manufacture. Lot number and manufacture date are printed on all packaging for traceability.
Q6: We are experiencing flow rate drift with our current silicone tubing after approximately 200 hours. What is causing this and how can it be fixed?
A: Flow rate drift after 200 hours typically indicates one of three issues: (1) high compression set in the tubing material — the tubing is not fully recovering between compression cycles; (2) incorrect hardness for your pump's occlusion setting — tubing that is too soft deforms excessively; or (3) dimensional inconsistency — ID variation between lots causes apparent flow drift when tubing is replaced. Send us a sample of your current tubing and your pump specifications, and our applications engineering team will diagnose the root cause and recommend the correct specification.
Q7: Can you provide pump tubing that is already sterilized and ready for use in a cleanroom environment?
A: Yes. We offer EtO-sterilized and gamma-sterilized pump tubing, individually packaged in peel-open sterile pouches with sterilization lot documentation. Sterile pump tubing is produced in our ISO Class 7 cleanroom and packaged under cleanroom conditions before sterilization. Lead time for sterile pump tubing is typically 3–4 weeks from order confirmation (including sterilization processing and sterility release testing).
Q8: We need pump tubing with a specific color code to match our device's tube identification system. Can you produce colored silicone pump tubing?
A: Yes. We produce pump tubing in a full range of colors using FDA-compliant, biocompatibility-tested pigments. Standard colors include clear, blue, red, green, yellow, white, and black. Custom colors can be matched to your Pantone or RAL specification. Color does not affect the mechanical or biocompatibility properties of the tubing — all colored grades use the same platinum-cured silicone base compound and carry the same certifications as clear tubing.
Ready to Qualify Chensheng Medical Pump Tubing?
Whether you are qualifying a new pump tubing supplier, troubleshooting performance issues with your current supply, or developing a new pump-based medical device, our applications engineering team is ready to help.
What we offer:
Free samples for qualification testing — standard sizes dispatched within 2 business days
Full technical documentation: TDS · CoA · ISO 10993 reports · USP Class VI reports · 21 CFR 177.2600 compliance
Custom size development — new extrusion tooling in 5–10 business days
Applications engineering consultation — pump compatibility, specification selection, failure analysis
Factory audit welcome — on-site or remote
→ Request Pump Tubing Samples→ Get a Custom Size Quotation→ Explore Our Medical Silicone Tubing Range
Related Articles:
Platinum-Cured vs. Peroxide-Cured Silicone: Which Should You Choose?
How to Choose Medical Grade Silicone Tubing: A Practical Guide for Healthcare Buyers
Custom Medical Silicone Products: The Complete OEM/ODM Process From Concept to Delivery
How to Choose a Reliable Medical Silicone Manufacturer in China
Medical-Grade Silicone Tubing for Respiratory Circuits: Compliance Requirements